In the R&D of cast film extrusion using novel engineering plastics, maintaining material stability during high-temperature processing remains the central challenge. These advanced materials typically require processing temperatures between 250°C and 400°C, making them highly susceptible to molecular chain degradation and fluctuations in melt properties. Such issues frequently result in film scrapping due to discoloration, embrittlement, and excessive thickness deviations.
Drawing on hands-on laboratory experience in cast film extrusion, this article examines the root causes of high-temperature material failure and proposes three key adaptation strategies: precise screw configuration selection, strict temperature control, and synergistic optimization of process parameters.
Cast Film Extrusion: A Guide for Novel Engineering Plastics
1. Root Causes of Poor High-Temperature Stability
The molecular structure of novel engineering plastics inherently makes them prone to stability issues under high-temperature conditions. Three primary factors contribute to this problem.
Thermal Degradation of Molecular Chains: Most engineering plastics contain rigid structures such as aromatic rings and ether bonds. While these structures provide excellent high-temperature resistance, prolonged exposure can trigger chain scission or crosslinking. For example, when PEEK is processed above 380°C with a residence time exceeding five minutes, the rate of molecular chain scission increases by 10–15%. This leads to a 20–30% drop in melt viscosity and reduces the tensile strength of the cast film by 15–20%, causing surface yellowing.
Sensitive Melt Flowability: The melt flow rate (MFR) of engineering plastics is highly sensitive to temperature variations. A fluctuation of merely ±5°C can cause an MFR deviation of 10–15%. In laboratory cast film extruders with small processing capacities, even minor temperature fluctuations can cause uneven melt flowability, leading to die exit velocity fluctuations exceeding 8%. Consequently, film thickness deviation expands from ±2% to ±5%, accompanied by wavy edge defects.
High-Temperature Failure of Additives: Antioxidants and lubricants incorporated to improve processing performance are prone to volatilization or decomposition at high temperatures. Phosphate antioxidants used in PC processing gradually volatilize above 300°C, reducing the material’s resistance to degradation and causing “crazing.” Meanwhile, lubricant failure increases frictional resistance between the melt and the barrel or die, resulting in poor material discharge and surface scratches.
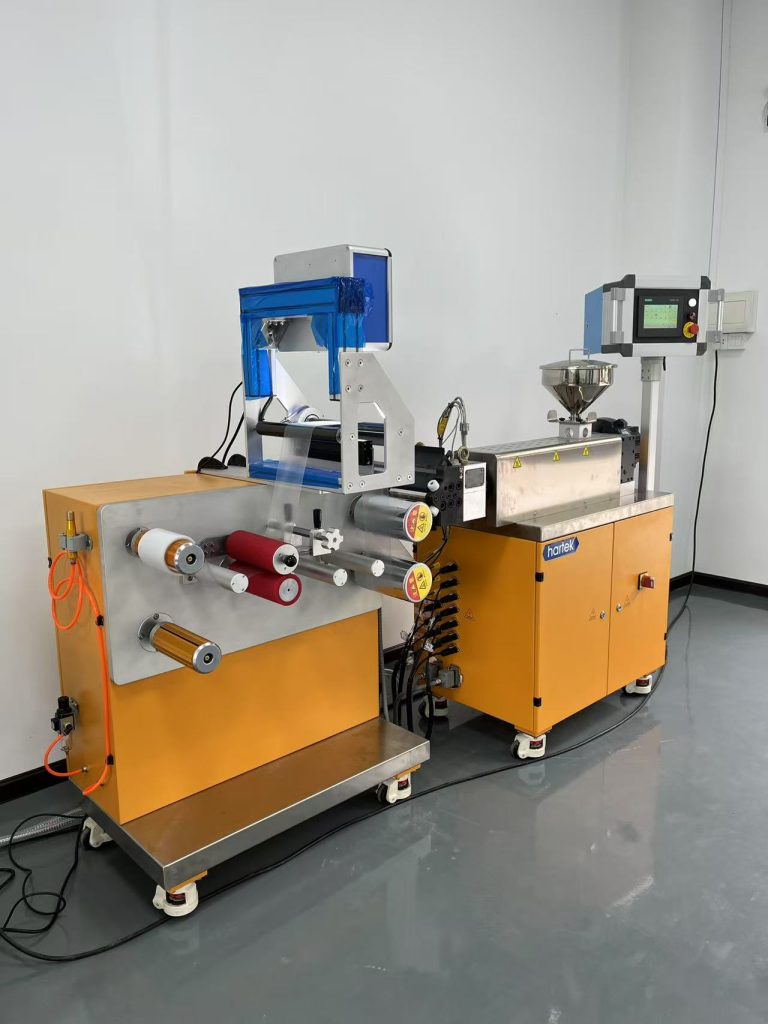
2. Adaptation Strategy 1: Precise Selection of Screw Configuration
The screw configuration directly impacts plasticizing efficiency, mixing uniformity, and residence time.
Selecting Screw Structure Based on Material Melting Characteristics: For low melt viscosity materials, a screw with a “gradually varying channel depth” is recommended. The channel depth gradually decreases from the feed zone to the metering zone to reduce shear intensity, preventing molecular chain degradation. Additionally, 2–3 sets of mixing elements should be incorporated to ensure uniform melt mixing. For high melt viscosity materials, a screw with a “suddenly varying channel depth” is required. The channel depth should decrease rapidly in the compression zone to enhance shear and plasticizing capability, while the metering zone should be lengthened to extend melt homogenization time.
Controlling Screw Length-to-Diameter Ratio and Residence Time: The L/D ratio of the screw in a laboratory cast film extruder should be controlled between 20 and 25. An excessively small L/D ratio can lead to insufficient plasticization, while an overly large ratio prolongs the melt residence time, increasing thermal degradation risk. For instance, when developing PEEK cast films, using a screw with an L/D ratio of 22, combined with a screw speed of 50–60 r/min, can keep the melt residence time within 4–6 minutes, reducing the molecular chain degradation rate to below 5%.
3. Adaptation Strategy 2: Strict Control of Temperature Precision
Temperature control is key to preventing high-temperature degradation. A precision control system must be established focusing on three aspects.
Segmented Temperature Control: The barrel should be divided into 3 to 5 independent temperature control zones, with gradient temperatures set according to material characteristics. For PI cast film R&D, recommended settings are: 300–320°C for the feed zone, 340–350°C for the compression zone, 360–370°C for the metering zone, and 370–380°C for the die head. Temperature deviation in each zone must be controlled within ±1°C.
Regular Calibration of Temperature Sensing Elements: Thermocouples and heating bands are prone to accuracy deviations due to prolonged exposure to high temperatures. Monthly calibration is required using a standard thermometer. If deviation from the set value exceeds ±1.5°C, the thermocouple must be replaced or heating power adjusted. Special attention should be paid to calibrating the die head temperature.
Real-Time Melt Temperature Monitoring: Install a melt temperature sensor at the die exit to monitor changes in real time. When temperature fluctuation exceeds ±2°C, an automatic warning is triggered. Experimental data shows that adding melt temperature monitoring can reduce the scrap rate due to film discoloration by 40–50% and keep thickness deviation within ±2.5%.
4. Adaptation Strategy 3: Synergistic Optimization of Process Parameters
Process parameters such as screw speed, extrusion pressure, and cooling rate must be matched synergistically.
Matching Screw Speed with Extrusion Pressure: For high-viscosity materials, a speed of 40–50 r/min is recommended, with extrusion pressure controlled between 15–20 MPa. For low-viscosity materials, speed can be increased to 60–70 r/min, with extrusion pressure maintained at 8–12 MPa. Screw speed should be adjusted in increments of no more than 5 r/min at a time.
Adapting Cooling Rate to Melt Temperature: Materials processed at high temperatures require “gradient cooling”: the first cooling roll section should be set to 120–150°C, the second to 80–100°C, and the third to 40–60°C. This gradual reduction minimizes warpage and deformation. For medium-temperature materials, “rapid cooling” can be adopted by setting the cooling roll temperature to 60–80°C.
Aligning Raw Material Pre-treatment with Processing: Engineering plastic pellets must be dried at 120–150°C for 4–6 hours to ensure moisture content of ≤0.02%, preventing film bubbles. For modified engineering plastics, a dedicated feed hopper should be used to avoid uneven melt mixing due to fiber agglomeration.
 English
 Arabic
 German
 Spanish
 French
 Russian